Just throwing this in the mix in case it is useful. I have a CNC that I use for hobbiest reasons and I would be willing to work with people (a few) to mill the baffle and perhaps baffle corners. I am in Albuquerque, NM US. I am not a machinist or a machining business, but do have 5 years experience on a Onefinity Journeyman. I am self taught, so there are still plenty of gaps in my knowledge. DM me if you want to chat about possibilities. That being said:
I spent a couple hours playing around at optimizing cutting paths last night and wanted to share some observations about why this project might not work for commercial businesses. The first is that it took me a couple hours to really get a good cut paths generated. I knew this looking at the project, but didn’t have the free “fun” time to explore until now. That’s a big hit for a business on a one off project. The machining time, even for MDF/Plywood/Hardwood is pretty high. My first roughing passes would take over an hour. I haven’t fully optimized the finishing passes, but total time looks like 2-4 hours. It is a two sided machining job meaning it takes very precise positioning while flipping the piece, that simply takes time either in the care of positioning/clamping or in the building of a jig to automate positioning/clamping, and all of that time has to paid for by just the cost of one piece.
The baffle could be redesigned to make it take significantly less time, but that would also likely impact the quality of the speaker a bit. Looking at the design, this is clearly a cost no object design. Things that I would change to make it faster while keeping the most important design features:
Make it machinable from one side. This could be done by changing the woofer cutout and countersinking. Getting rid of the countersinking is a pretty minimal savings machine time wise but would have to be done to cut the repositioning time out. The bevel of the rear woofer cutout is where most of the machine time for that side is occurring. This is because it is sloped (meaning only a tiny part of a standard flat end mill is being used and any given time) and complexly shaped. I am assuming the bevel is due to the depth of the baffle (57mm) and airflow needs. It would save a ton of machine time to step this like the tweeter, even more to redesign so it could be cut from the front, but I imagine that impacts sound quality.
Depth. The depth of the baffle (57mm) has a few consequences. First, in the US, it means gluing three pieces of MDF or plywood together to get that depth if you’re going COTS for those. It’s also an awkward size for wood slabs. The depth also causes issues in bit selection in that in the US one would normally use 1/4 or 1/8 inch. The through holes would mean picking a 1/8. The problem is 1/8 bits tend to have low overall length for strength reasons meaning the collar of the router (in my case) starts hitting the stock. This can be overcome by drilling halfway from both sides, but that increases precision requirements or by sourcing a rarer more expensive longer bit.
The front presents fewer machining issues, but the curves mean longer machining times, at least for a great finish.
Getting to a one sided machining design, would be a lot of redesign but is probably doable (by me) if one excepts the (unknown) loss of sound quality. But even just lowering the finish level could make it doable from my perspective. If the recipient is willing to sand, the design could be machined with a 1/4 inch bit and “finished” with an 1/8th. Or even just shaped with a 1/4 if the recipient agrees to drill the through holes themselves.
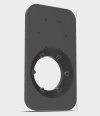
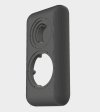
Anyway I am including a couple of pics of a simulated machining with just 1/4 and 1/8 bits that optimizes for minimum machine time. It is still about 2 hours on the CNC. Anyway I am interested in working with someone (a couple people) to try and figure something out. Not as a business but in the interests of developing my skills further and maybe something in barter for the time and materials.